Automation Solution Engineering
SPM · HYDRAULIC · PNEUMATIC · CONVEYOR · PANELS
Press-fitting is one of the most common assembly operations in engineering. A bearing is pressed into a housing, a bush into an arm, a pin into a hole. Done badly, the part can be damaged, misaligned or too loose. Done well, it is repeatable and easy to check. This guide compares the three main press types used in a press-fit assembly machine and shows what to specify.
| Type | Strengths | Limits |
|---|---|---|
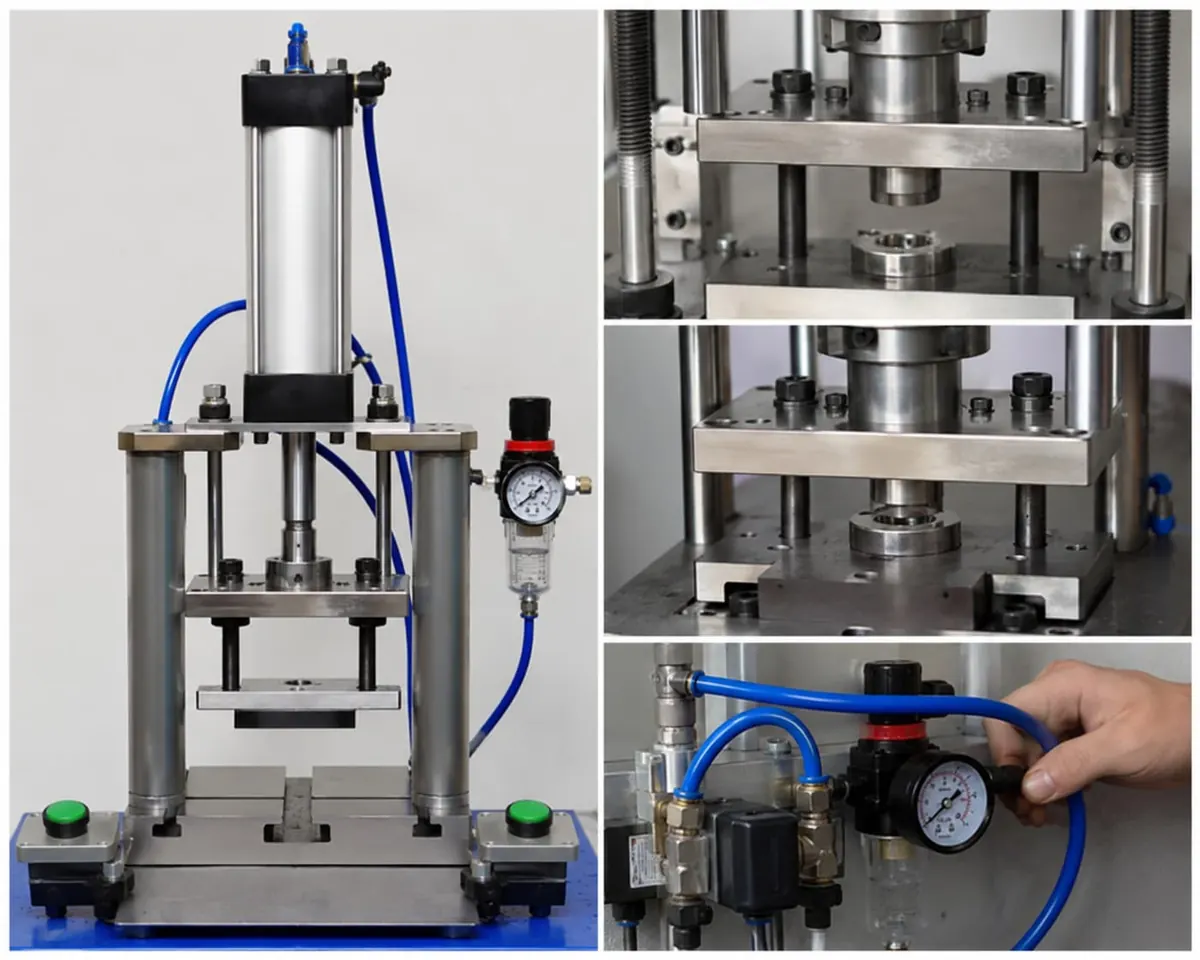
| Pneumatic press | Fast cycle, clean, low maintenance, needs only compressed air, good for light parts | Lower force, force follows air pressure, less precise speed control |
| Pneumo-hydraulic press | Higher force from an air supply, smoother pressing than plain pneumatic | Moderate cycle speed, more parts to maintain than pneumatic |
| Hydraulic press | High force at any stroke position, long stroke, good for heavy fits and forming | Needs a power pack, oil maintenance, slower than pneumatic |
| Servo press | Precise position and force control, full pressing curve, very repeatable | Higher initial cost, needs more programming skill |
Our pages on pneumatic presses and hydraulic presses describe the options we build, and the article pneumatic vs hydraulic press goes deeper into the comparison.
The pressing force depends on the interference between the parts, the contact length, the materials, the surface finish and any lubrication. The safest way to set the force is to test with real parts and measure. Then choose a press with enough margin above the measured peak force, so it is not working at its limit every cycle.
A basic machine only presses to a stroke or pressure setting. A better one measures what actually happens:
This catches a missing part, a damaged bore, an oversize shaft or a part not fully seated, none of which an operator can feel reliably.
Most press-fit problems come from the fixture, not the press. The lower fixture must support the part without distorting it, and the upper tool must push on the right surface and stay square. Guide pins or a guided ram, a nest that locates the part and a stop that sets the final depth all help. Tell us if your parts vary, because a fixture that suits one variant may need adjustment for another.
Automation Solution Engineering builds press-fit and assembly SPM machines with pneumatic, pneumo-hydraulic, hydraulic or servo actuation, with two hand or light curtain safety and PLC control. Force and position monitoring and reject handling can be added on request. See our SPM machines page or read the complete SPM guide.
Press-fit assembly joins two parts by pressing one into the other with an interference fit, so friction holds them together. Common examples are bearings pressed into housings, bushes into arms and pins into holes.
Choose pneumatic for light parts and fast cycles, hydraulic when you need higher force and long stroke, and servo when you need precise control of position and a full force-versus-displacement record. Many jobs are best served by a pneumo-hydraulic press that gives more force from an air supply.
Yes. With a load cell and a position sensor the machine can check that the force stayed within a window and the part reached the correct depth, and it can reject a part that falls outside.